- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
Cold Chain Packaging Bags
2. Rigid structure maintains shape under load
3. Good low-temperature resistance for cold chain
4. Versatile packaging for multiple scenarios
5. Direct factory supply with consistent quality
Cold Chain Packaging Bags - Professional Temperature-Controlled Transport Solutions for Perishable Logistics
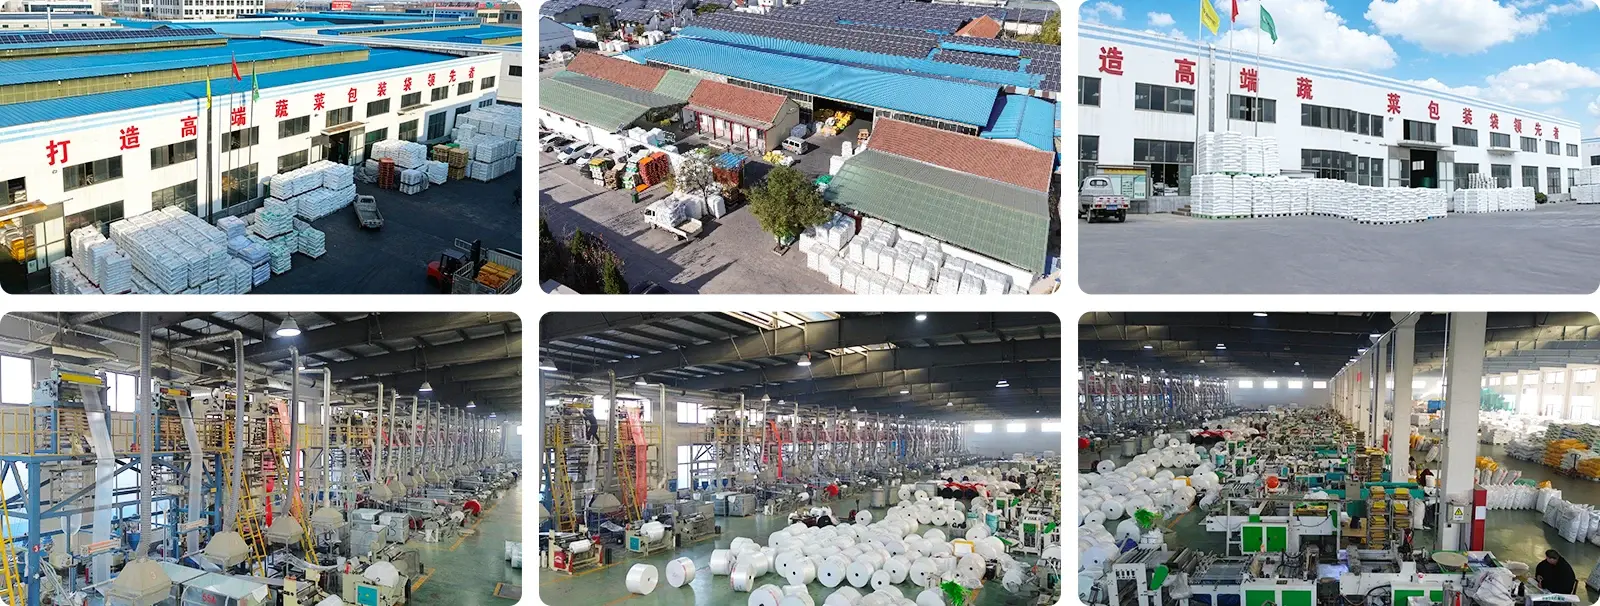
Temperature stability is the core guarantee for the logistics transportation of pharmaceuticals, biological specimens and fresh food products. Reliable insulated packaging can effectively avoid product deterioration and efficacy loss caused by temperature fluctuations. Rizhao Luming Plastic Technology Co., Ltd. specializes in the production of high-performance Cold Chain Packaging Bags. Relying on a 12,000 ㎡ professional production base, more than 100 sets of production equipment and a professional team of over 120 employees, we maintain a stable monthly output of hundreds of millions of pieces.
What Makes Professional Cold Chain Packaging Essential
Temperature-sensitive goods face huge quality risks during long-distance transportation and cross-regional distribution. Ordinary traditional packaging cannot cope with complex ambient temperature changes, which often leads to product loss. Different from ordinary packaging, our professional cold chain bags adopt composite materials such as high-reflection metalized film and high-density foamed polyethylene to effectively block heat transfer.
This professional structural design solves three major pain points of cold chain logistics. Firstly, it effectively avoids temperature deviation, keeps goods within the safe temperature range, and ensures product activity and freshness. Secondly, compared with rigid insulation containers, the lightweight design greatly reduces overall shipping costs. Thirdly, the foldable and collapsible structure saves a lot of warehouse storage space and reduces inventory management costs.
High-value temperature-sensitive products need matching high-standard packaging protection. Whether it is vaccines and biological reagents that require 2°C–8°C constant temperature storage, or frozen seafood and fresh ingredients for e-commerce distribution, our professional insulation packaging can effectively prevent spoilage and maintain consistent product quality standards.
Technical Specifications and Material Composition
All our cold chain packaging bags adopt precision industrial formula and layered composite technology, with clear and reliable performance parameters to meet the inspection standards of professional cold chain logistics:
| Parameter | Specification | Performance Benefit |
|---|---|---|
| Primary Material | Virgin HDPE | Food-grade safety, no toxic leaching |
| Reflectivity Rate | >95% | Deflects infrared radiation effectively |
| Thermal Conductivity | Low K-value | Minimizes heat gain during transit |
| Tensile Strength | High-grade | Prevents punctures and tears |
| Temperature Range | -78.5°C to +40°C | Compatible with dry ice to tropical heat |
| Seal Type | Airtight zipper/adhesive | Ensures complete thermal closure |
| Moisture Barrier | Multi-layer vapor shield | Protects against humidity intrusion |
The overall seamless composite structure eliminates structural weak points and avoids temperature control failure caused by local gaps. We support fully customized sizes, with load-bearing specifications ranging from 5kg to 35kg. The professional surface waterproof treatment ensures flexible use while completely isolating external water vapor.
Cold Chain Packaging Bags Applications
Medical and pharmaceutical cold chain logistics have extremely strict safety and stability requirements. Vaccines, insulin preparations and biological drugs will lose their efficacy and activity once they deviate from the specified temperature range. Biological samples need to maintain stable storage conditions from production, transportation to clinical use.
Our Cold Chain Packaging Bags can stably maintain a constant temperature environment of 2°C–8°C even in extreme high and low temperature environments. The outer metalized reflective layer isolates external heat radiation, and the inner insulation layer stabilizes the internal microclimate. It can be used with ice packs and phase change refrigerants to achieve long-term constant temperature protection.
Suitable for the transportation of clinical trial samples, blood samples and biopsy specimens, the multi-layer isolation structure forms a safe secondary protection barrier. The product fully complies with IATA Category B biological substance transportation specifications, meeting the compliance requirements of global cross-border logistics.
Stable temperature control performance ensures that all medical supplies and biological reagents arrive intact, effectively guaranteeing the safety of medical and clinical application.
Fresh Food and E-Commerce Logistics Solutions
With the rapid development of fresh e-commerce, end customers have higher and higher requirements for the freshness of frozen meat, seafood, chocolate and other temperature-sensitive ingredients. Stable insulation packaging has become the key to improving customer satisfaction.
Our cold chain insulation bags perfectly solve the 24–48 hour insulation and fresh-keeping pain points of B2C terminal distribution. It can effectively prevent frozen goods from thawing during last-mile delivery, and avoid product damage and appearance deterioration caused by condensation.
In the whole link of fresh produce transportation, it locks the moisture and nutrition of fruits and vegetables, and prevents frozen products from freezer burn and quality deterioration. Different from bulky rigid insulation boxes, the lightweight design reduces the dimensional weight of goods and effectively saves logistics costs for e-commerce sellers.
Strong environmental adaptability can cope with high temperature in summer and low temperature in winter. Matching different refrigerants can realize stable transportation of temperature-sensitive goods in all seasons.
Quality Assurance and Performance Testing
All our cold chain packaging products have passed strict international standard tests to ensure stable and reliable batch performance. The whole production process is supervised by standardized inspection procedures.
All products have passed leak-proof test and food-grade safety evaluation, complying with FDA and EU 10/2011 food contact standards. Supported by ISO 9001 quality management system, every batch of products has stable and traceable quality.
Customization Options and Sustainability Features
We also offer complete dimensional customization services such as custom size, color matching and brand logo stamping. Custom packaging is helping businesses to define brand image and boost terminal brand exposure throughout the distribution process.
We can build special structural specifications based on client product dimensions, weight and transportation cycle, encompassing small-batch medical reagent packing and large-batch frozen food bulk transportation situations.
Frequently Asked Questions
Q1: How long can the cold chain bags maintain stable temperature control?
A1: The insulation duration ranges from 12 to 48 hours, depending on bag thickness, insulation structure and refrigerant dosage. We support customized ISTA environmental testing to match your actual logistics cycle.
Q2: Are these cold chain bags reusable and recyclable?
A2: The heavy-duty reinforced version supports multiple cyclic uses. Standard bags are made of recyclable plastic materials and can be put into professional recycling streams to meet circular economy requirements.
Q3: Can the bags be used with dry ice for ultra-low temperature transportation?
A3: Yes. The material can withstand ultra-low temperature down to -78.5°C without cracking or embrittlement, fully suitable for dry ice cold chain transportation scenarios.
Q4: What are the advantages compared with traditional EPS foam coolers?
A4: It achieves equivalent insulation performance, while saving 80% storage space and greatly reducing shipping dimensional weight, effectively lowering your overall logistics costs.
Q5: Can the bags block external moisture and condensation?
A5: Yes. The multi-layer composite structure forms a high-efficiency vapor barrier, which can isolate external humid air and prevent internal refrigerant failure and product moisture damage.
Contact Rizhao Luming Plastic Technology
Feel free to contact our Cold Chain Packaging Bags sales team via sales@lumingplastic.com to get professional technical consultation, free samples and exclusive bulk quotations.
Get customized packaging solutions with fast professional support.