- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
Black HDPE Produce T-Shirt Bags
2. High rigidity, maintains shape without sagging
3. Water and moisture resistant, keeps contents dry
4. Designed for produce and fresh food packaging
5. Direct factory supply with consistent quality
6. Multiple sizes and grammages available, fully customizable
Black HDPE Produce T-Shirt Bags - Premium Heavy-Duty Packaging Solutions for Commercial Applications
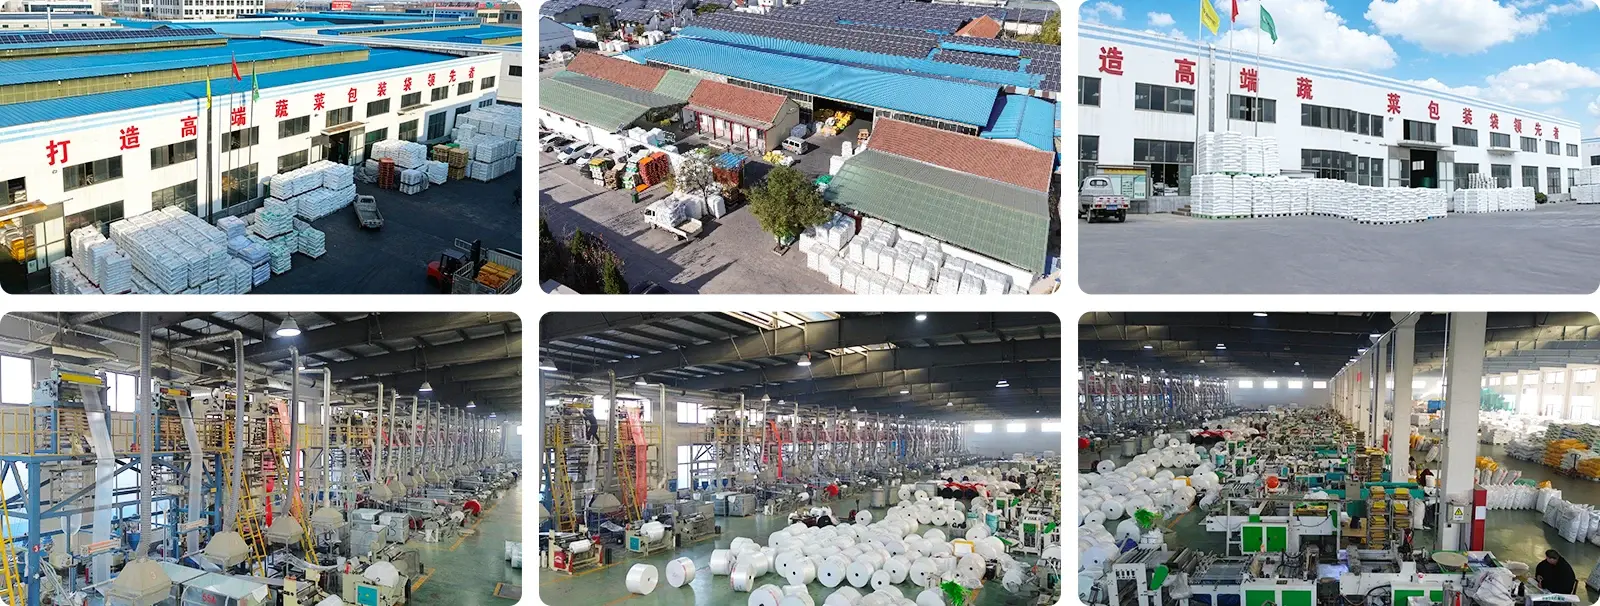
Rizhao Luming Plastic Technology Co., Ltd. manufactures Black HDPE Produce T-Shirt Bags engineered for demanding commercial environments. Operating from a 16,500 m² production facility with over 100 sets of advanced equipment, our company delivers hundreds of millions of vegetable packaging bags monthly. These bags utilize virgin food-grade HDPE resin with density ranging from 0.941 to 0.965 g/cm³, offering load capacity from 5kg to 35kg per unit depending on specifications. The integrated vest handle design ensures seamless stress distribution, while the carbon black formulation provides complete opacity and UV protection for light-sensitive products.
Why Choose High-Density Polyethylene for Your Packaging Needs
The material design of these bags overcomes major problems in the industry. HDPE has a good strength-to-weight ratio so we can work with thinner sheets without losing durability. The "moisture barrier" ensures that the product stays dry throughout transit and storage.
Black carbon masterbatch does not just add color. It enhances the molecular framework for puncture resistance over transparent films and filters UV light to protect packed items from light damage.
Load requirements permit film thickness of 8 to 25 microns. It has excellent crystallinity which delivers good rigidity and maintains the bag's form while filling and handling. Resistance to acid and alkali to safeguard contents under various operating circumstances.
Technical Specifications and Performance Parameters
| Property | Specification | Test Standard |
|---|---|---|
| Material Density | 0.941-0.965 g/cm³ | ISO 1183 |
| Film Thickness | 8-25 microns | ASTM D2103 |
| Load Capacity | 5-35 kg (size dependent) | Internal Testing |
| Melting Point | Approx. 130°C | DSC Analysis |
| Opacity | 100% light blocking | Spectrophotometer |
| Temperature Resistance | -50°C to +80°C | ASTM D1709 |
| Handle Type | Integrated vest design | Seamless construction |
These parameters ensure reliable performance across temperature fluctuations and rough handling conditions. The heat seal strength undergoes rigorous testing because black masterbatch can affect thermal bonding. Our quality protocols verify that bottom seals exceed film strength to prevent blowouts.
Enterprise-Grade Manufacturing Standards
Quality inspections are carried out at all stages of manufacture. Dart impact testing to ASTM D1709 checks for resistance to knocks and drops in transit, and tensile tests demonstrate that handles stand up under full load.
Heat seal strength is a primary emphasis of the QA. A spectrophotometer is used to measure the carbon black dispersion, to eliminate thin, light-leaking patches and guarantee that each batch has the same opacity.
Each batch is tested for elongation in accordance with ASTM D882. This means the film will stretch correctly under weight without ripping.
Our 120+ production team checks on film structure at all times to ensure uniform dimensions.
Black HDPE Produce T-Shirt Bags Applications
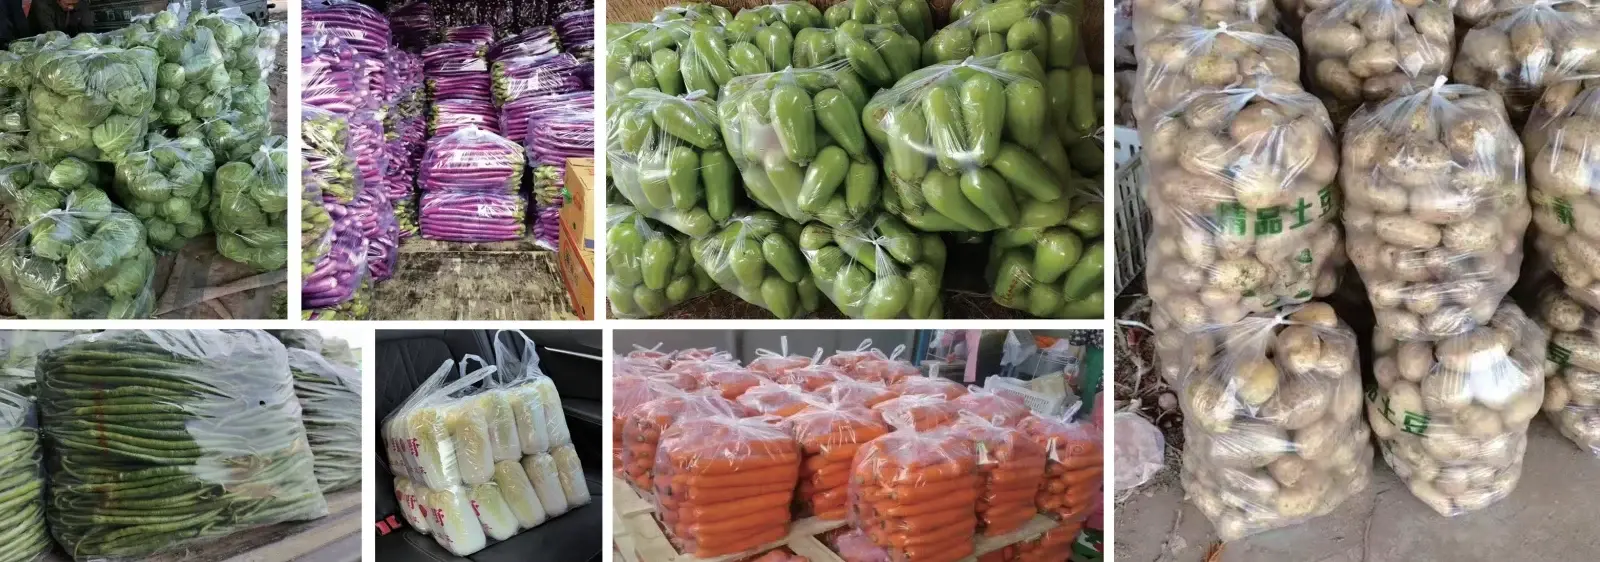
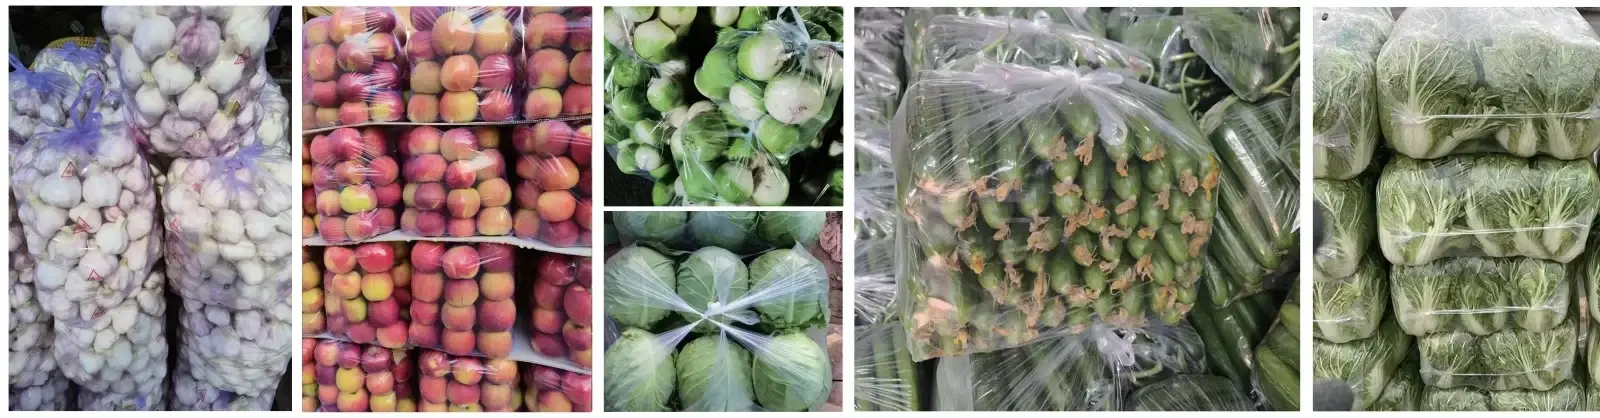
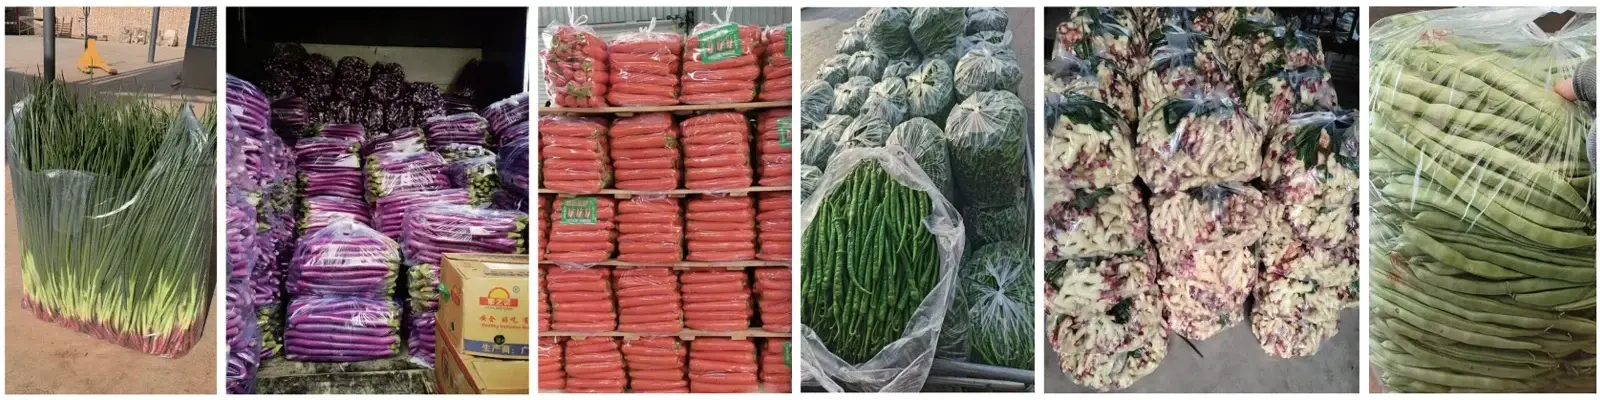
These bags are used by farms for potatoes, ginger, and other root crops. "Complete darkness inhibits sprouting and solanine synthesis caused by light. Wholesalers get their power by moving in bulk.
Black HDPE t-shirt bags are used by industrial users for car parts and hardware. Grease is concealed by opacity, sharp metal is handled by puncture resistance, and inventory is protected.
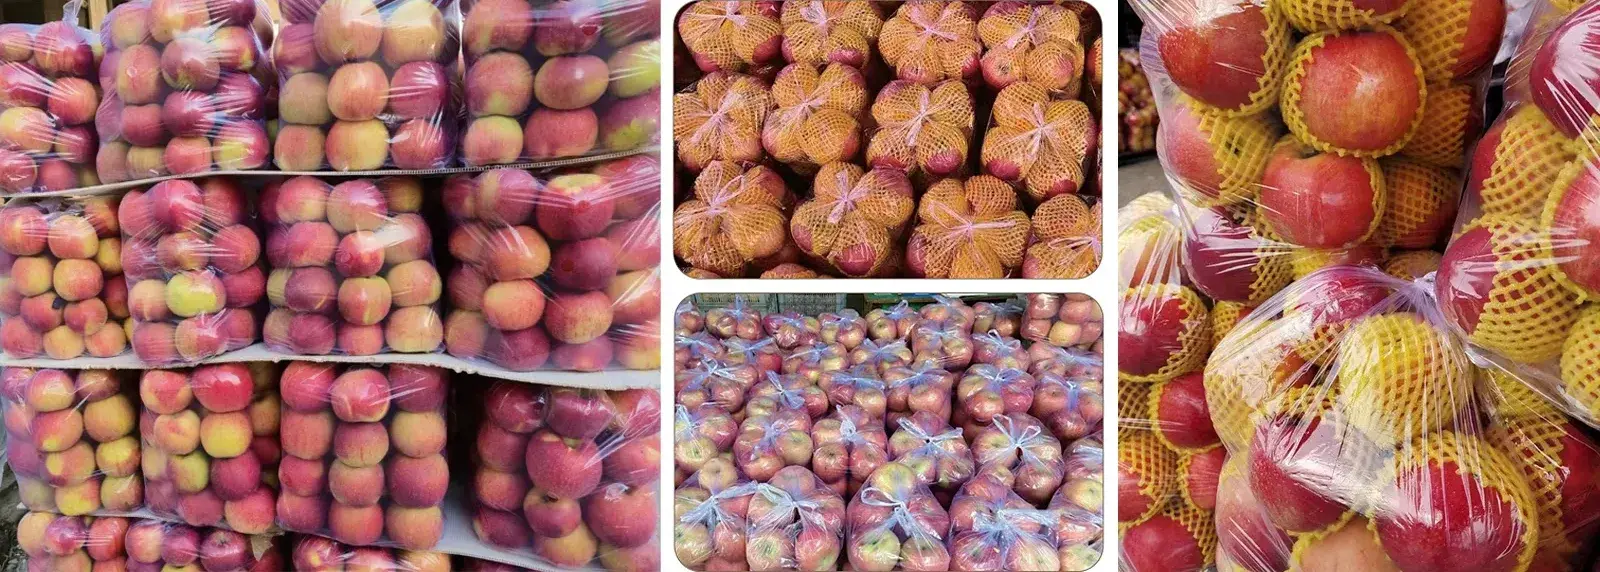
Retailers employ them to protect high value items. They are used as heavy duty liners for moist items in waste facilities. They work consistently down to -50 degrees C in cold storages.
Customization Options and Bulk Ordering Advantages
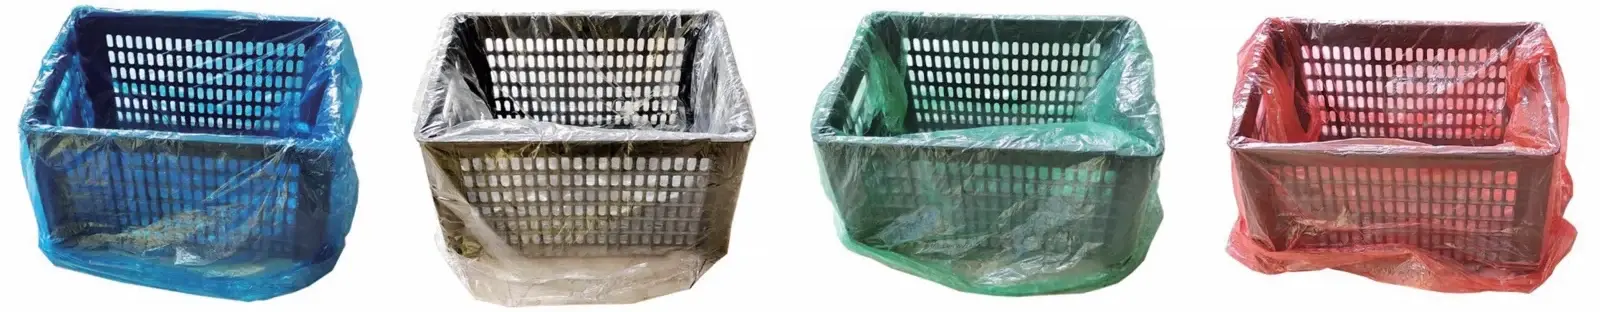
Custom sizes, thicknesses and logo printing are available, colors are available on MOQ.
Factory direct price on bulk orders. Consistent supply due to strong monthly production. 8 domestic shops that support locally.
We can customize melt index for your filling machine and modify handles for load. R&D tailors bag parameters to your use scenario.
Environmental Considerations and Recycling Information
These bags have Resin Identification Code 2 and are compatible with HDPE recycling systems. Be aware that carbon black may interfere with automatic sorting at recovery plants. They count as recyclable plastic for sustainability reporting.
Down-gauging is the use of less material without losing load strength. Less fuel use for transit due to lighter baggage
Our food-grade products are FDA approved for produce and dry items. Safe to use from farm to retail, no dangerous ingredients migrate into contents.
Frequently Asked Questions
Q: Does the black pigment compromise food safety?
A: When manufactured with FDA-compliant, food-grade carbon black masterbatch, these bags are completely safe for produce and dry goods. Our formulations use certified additives that meet international food contact standards.
Q: Why do these bags have a crinkly texture?
A: The characteristic texture comes from HDPE's high crystallinity, which provides the stiffness and strength needed for heavy loads at thin gauges. This property is what enables performance compared to softer plastic films.
Q: Are these bags recyclable through standard programs?
A: Yes, they fall under RIC 2 for HDPE recycling. However, the black pigment may affect automated sorting equipment at some facilities. Check with your local recycling program about their specific capabilities.
Q: What causes bottom seal failures in inferior products?
A: Blowouts typically result from improper melt flow index settings or insufficient heat during sealing. Our professional-grade bags undergo batch testing where seal strength must exceed film strength before release.
Contact Us for Your Packaging Solution
Ready to upgrade your Black HDPE Produce T-Shirt Bags packaging performance? Reach us at sales@lumingplastic.com for technical specifications, pricing, and sample requests.
Get customized packaging solutions with fast professional support.